Industrial Chemical Processes and Fluid Transfer
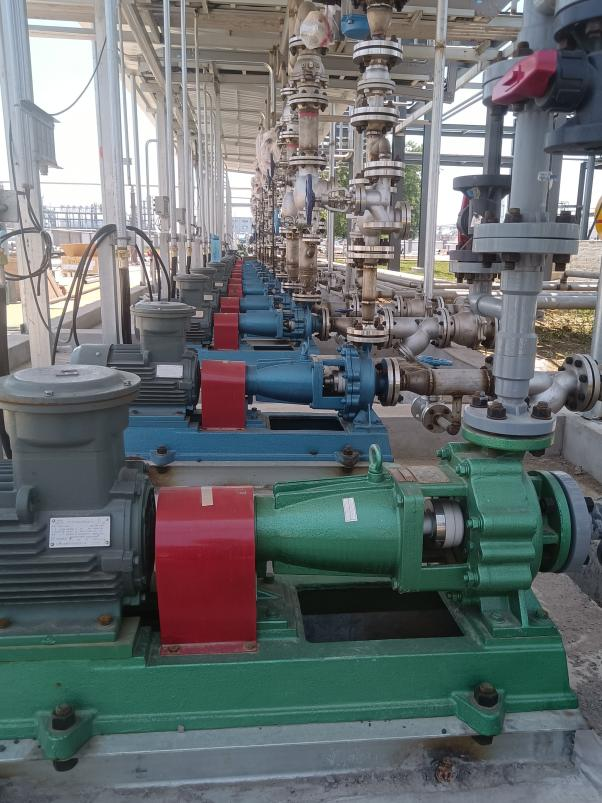
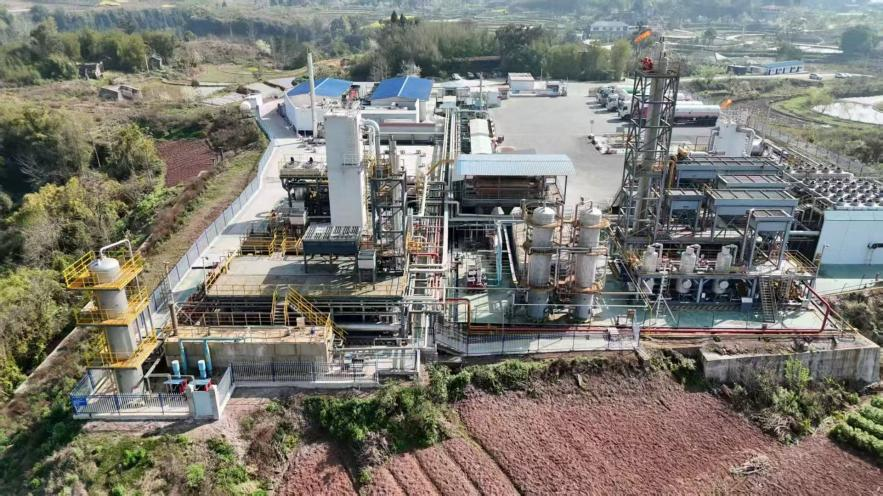
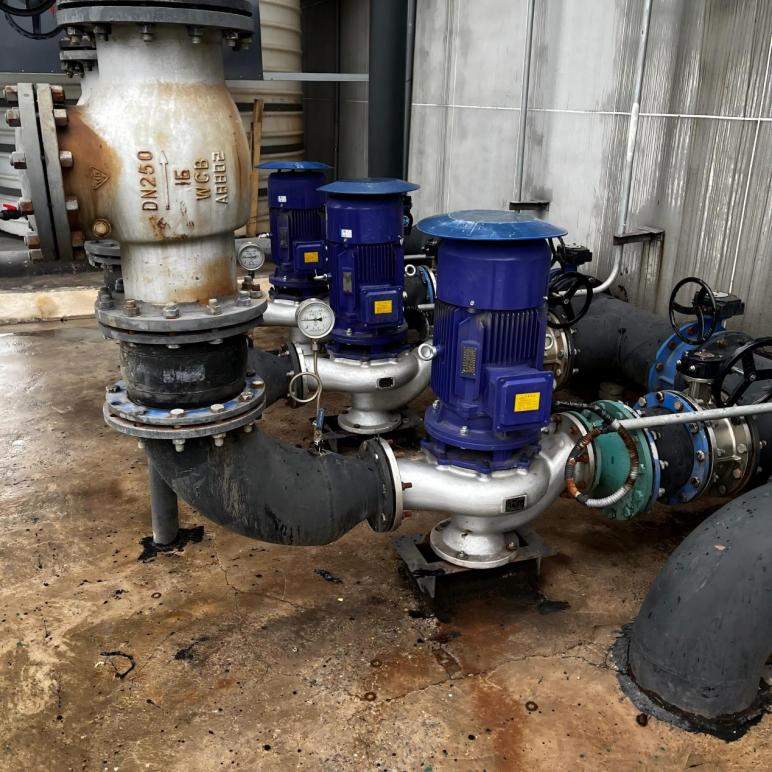
In large-scale chemical processing plants, petrochemical complexes, and fine chemical industrial parks, rows of heavy-duty horizontal chemical pumps stand as the vital "heart" of the facility's fluid transfer and process circulation systems. Engineered specifically to withstand severe and demanding industrial environments, this series of chemical pumps excels in the following critical applications:-
Corrosive Chemical Transfer: Designed for the safe, smooth, and efficient handling of strong acids, alkalis, salt solutions, organic solvents, and other highly corrosive media.
-Process Circulation and Pressurization: Provides reliable system pressure boost and material circulation for continuous production lines such as synthetic resins, petroleum refining, and fertilizer manufacturing.
-Tank Farm Loading/Unloading and Wastewater Neutralization: Meets the rigorous demands of rapid chemical loading/unloading in storage areas, as well as the transport and neutralization of high-salinity and corrosive industrial wastewater within the plant.
Horizontal Chemical Pump vs. Magnetic Drive Pump
-Structure & Sealing: Horizontal chemical pumps utilize traditional mechanical seals, which require cooling water or flush liquid for protection. In contrast, magnetic drive pumps use a magnetic coupling and containment shell to achieve complete sealing and zero leakage.
-Medium Compatibility: Horizontal chemical pumps are suitable for the vast majority of acid, alkali, and salt solutions. However, when handling highly toxic, flammable, explosive, or extremely valuable chemicals where absolute leak prevention is required to avoid safety hazards, magnetic drive pumps are typically compared and chosen as the preferred option.