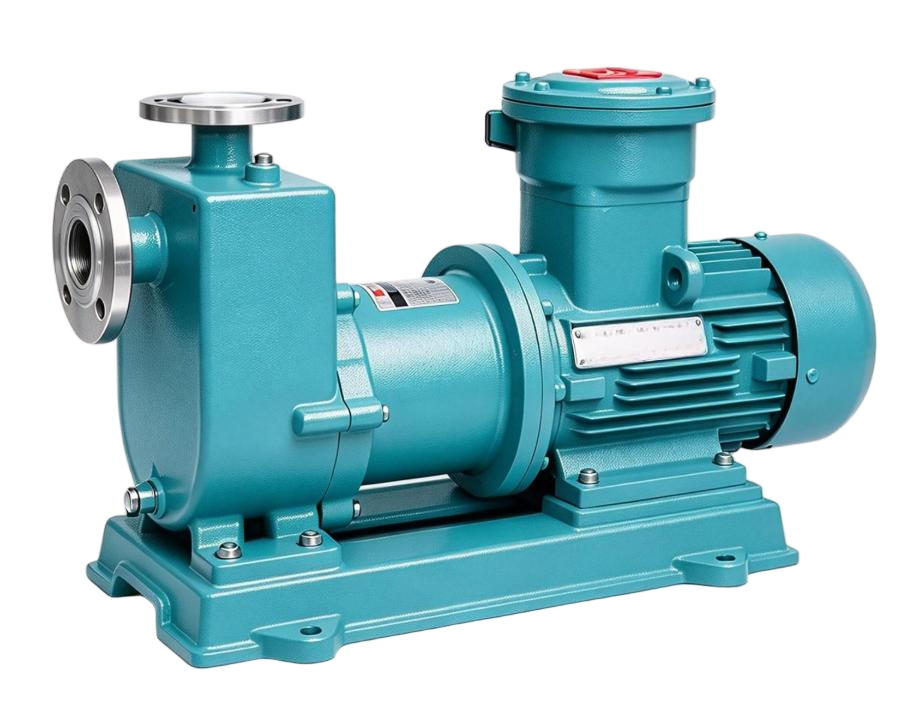
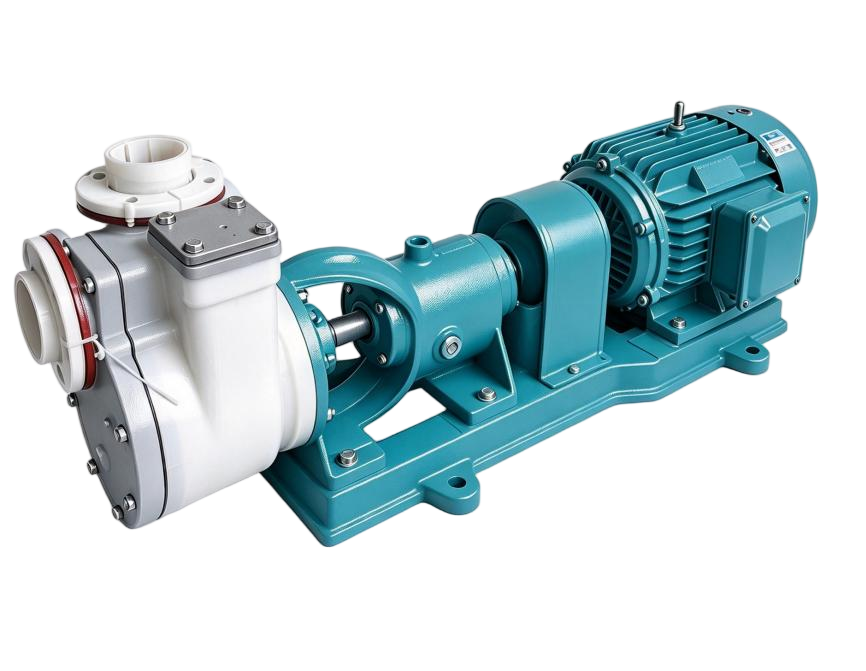
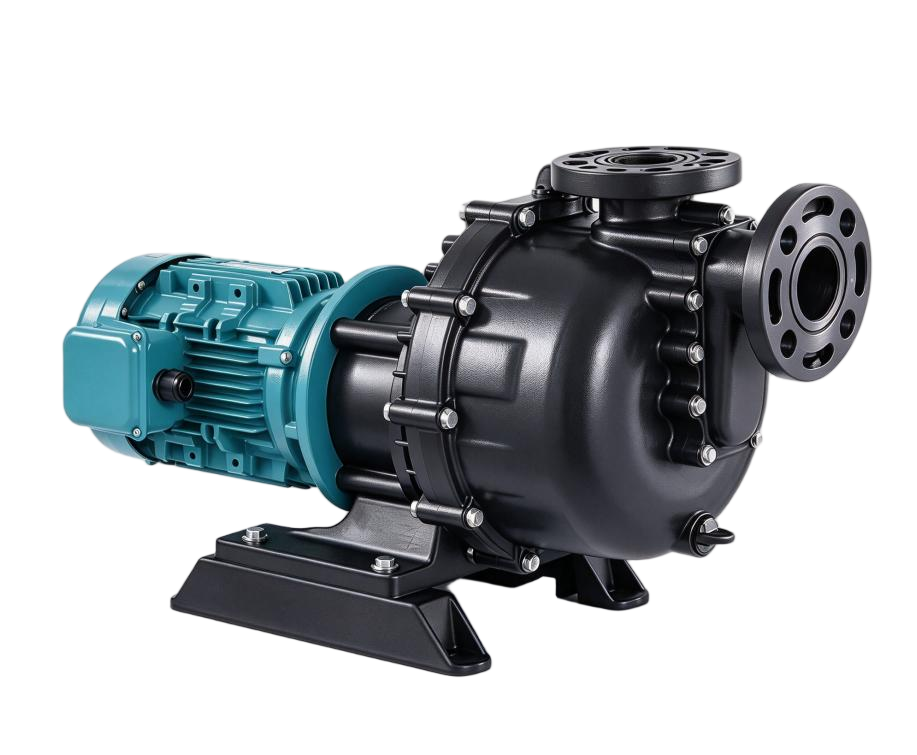
-Chemical Compatibility & Advanced Materials: Specially engineered for acids, alkalis, organic solvents, and corrosive chemical fluids. Constructed from top-tier corrosion-resistant materials such as fluoroplastics and 304/316 stainless steel, it handles strong corrosive media that standard pumps cannot tolerate.
-Sealless & Zero Leakage Design: Widely utilizes magnetic drive or close-coupled seal-less structures to drastically reduce leakage risks. It satisfies stringent sealing and safety requirements for flammable, explosive, toxic, hazardous, and high-value chemical media, meeting the highest safety standards for chemical applications.
-Complex Condition Capability & Multiphase Handling: Features powerful self-priming suction lift, multiphase mixing, or automated priming performance. It directly resolves key pain points in complex industrial fluid delivery—such as handling easily vaporized liquids, gas-entrained media, and high suction lift requirements—making it ideally suited for harsh operating conditions in chemical, pharmaceutical, pickling, and electroplating industries.